
Slippery Kitchen Floor: Fixing It Properly, Not Quickly
A slippery kitchen floor is one of the most persistent hazards in UK catering. Hot oil, animal fat and soapy wash water settle on quarry tiles every shift. Traction then disappears. Duckboards and generic floor paint do not fix the problem. Kitchens need a seamless system built for mechanical traffic, daily washdowns and constant chemical attack.
Cleaning chemicals cannot restore grip once the surface profile has gone. Mats and coatings only postpone the accident, the enforcement notice and the injury claim. So why do standard slip prevention methods collapse under a busy service? What does a permanent, fully compliant specification actually require?
Key Takeaways
- Pendulum testing with clean water alone fails to show how hot oils, animal fats and detergents behave underfoot during service.
- Rubber mats and surface floor paints give short-term relief whilst trapping grease, harbouring bacteria and creating serious secondary trip hazards.
- Heavy duty polyurethane screeds hold their slip resistance and absorb thermal shock from steam cleaning and boiling spills to 120 degrees.
- Regulation 12 requires floors to be suitable and not slippery, so known hazards must be engineered out rather than signposted.
- Lasting floor integrity depends on diamond grinding back to sound concrete, not chemical treatments or new coverings over worn tiles.
Slip Prevention Methods Compared on Lifespan and Grip
Catering operators usually reach for the cheapest available fix when a floor turns dangerous. Setting those measures against engineered resin systems exposes a wide gap in lifespan, hygiene performance and real traction under heavy contamination. The table below shows how each common intervention behaves across a full week of hot service.
Tapes and duckboards cost very little to buy. Their short failure cycle then generates repeat labour, repeat spend and repeat accident exposure. A heavy duty polyurethane screed delivers engineered grip, thermal stability and a seamless hygienic surface. It resolves the operational problem that standard kitchen floor coverings were never built to handle.
| Intervention Method | Expected Lifespan | Slip Potential in Grease | Thermal and Chemical Durability |
|---|---|---|---|
| Intervention MethodRubber Duckboards and Mats | Expected Lifespan3 to 6 months | Slip Potential in GreaseHigh (collects grease beneath) | Thermal and Chemical DurabilityPoor; degrades under hot animal fats |
| Intervention MethodTopical Anti-Slip Floor Paint | Expected Lifespan1 to 3 months | Slip Potential in GreaseHigh (wears smooth quickly) | Thermal and Chemical DurabilityFails under thermal shock and caustic cleaners |
| Intervention MethodQuarry Tiles with Standard Grout | Expected Lifespan2 to 5 years (grout fails sooner) | Slip Potential in GreaseModerate to high as profile wears | Thermal and Chemical DurabilityPorous grout absorbs grease and rots |
| Intervention MethodPolyurethane Resin Screed (6 to 9 mm) | Expected Lifespan15 to 20 years | Slip Potential in GreaseLow (engineered PTV 36 or above) | Thermal and Chemical DurabilityWithstands steam cleaning and organic acids |

Flaws in Standard Water-Based Pendulum Testing
Clean Water Versus Kitchen Contaminants
Clean water testing does not reflect a working kitchen because cooking fat changes boundary lubrication. A micro-textured surface can displace thin water films. Warm vegetable oil and melted animal tallow behave very differently. Their higher viscosity builds a continuous hydroplaning film that blinds the tread pattern on standard catering footwear.
Grease mist, dairy spills and rendered fat coat every walkway in a busy kitchen. An operative stepping onto warm cooking oil meets a contaminant that bears no resemblance to mains water. Viscous lipids form a hydrodynamic wedge under the sole. The foot slides without resistance unless the finish has enough surface roughness to pierce that barrier. Clean-water certification therefore offers false comfort to any site manager facing daily oil deposits.
Pendulum Test Values and Risk Categories
The British Standard pendulum test measures slip resistance and produces a Pendulum Test Value. That figure quantifies pedestrian slip risk on the surface tested. HSE guidance treats a PTV of 36 or above as low slip potential. Readings of 24 or below indicate high slip potential, roughly a one-in-twenty chance of slipping.
The test to BS 7976 sweeps an engineered rubber slider across the floor to simulate a heel strike. Specifiers should insist on testing under representative site conditions. A factory-fresh tile may reach a PTV of 45 with clean water. Tested with cooking oil, the same tile often falls below 20. Genuine low slip potential is only proven against the contaminants actually present on the production line.
Why Quick Fixes Fail on a Slippery Commercial Kitchen Surface
Problems with Rubber Duckboards and Anti-Fatigue Mats
Duckboards and loose rubber mats create an illusion of safety and multiply real risk. Liquid grease, cooking starch and mop water gather beneath the unbonded mat. Hidden bacterial colonies follow. Mat edges then curl under trolley wheels and introduce a severe trip hazard along the busiest preparation lines.
Mats do not resolve a slippery commercial kitchen. They conceal it. Spilled oil runs straight through the perforations onto the surface below. Trapped fat stagnates, emulsifies and cannot evaporate, leaving an odorous slime. Staff moving hot-holding cupboards or ingredient bins catch the edges and ruck the mats into obstructions. Cleaning them means manual lifting, heavy handling and contaminated water dragged across clean preparation zones.
Rapid Wear of Thin Paints and Topical Sealers
Thin coatings and single-pack floor paints peel quickly over worn commercial tiles. These topical treatments measure only a few hundred microns. They lack the compressive strength and chemical bond needed for dropped utensils, drag loads, hot oil and the alkaline chemicals used in nightly cleaning.
Paint films rely on weak surface tension unless aggressive mechanical profiling comes first. Hot fat softens the resin matrix on contact. Dragged gastronorm containers and heavy stockpots score straight through the film. Washdown water then penetrates the scratched edges within weeks. Delamination follows, and flaking paint chips become a foreign-body contamination risk in food preparation areas.
Did You Know?
Slips, trips and falls on the same level caused 30% of all non-fatal employee injuries reported under RIDDOR in 2024/25. They remain the single largest reported accident kind in Great Britain, according to HSE statistics.
Substrate Degradation Beneath Quarry Tiles and Grout Lines
Capillary Action and Trapped Grease Beneath Tiles
Worn quarry tiles fail as grout lines crumble and absorb fat, water and caustic chemicals. Moisture then penetrates the joints. Organic matter rots beneath the bed, the setting mortar softens and chemical adhesion to the substrate breaks. Tiles begin to rock, crack and lift during service.
Quarry tiles are dense, but cementitious grout stays porous. Cooking oil seeps into the grout matrix by capillary action over months of production. Aggressive degreasers dissolve the cement binder. Joint lines erode into troughs that pool dirty wash water. Once that water reaches the adhesive bed, the bond fails. Hollow, loose tiles then pinch footwear and hold biological waste that surface scrubbing cannot reach.
Mechanical Grinding for Substrate Restoration
Mechanical preparation is essential before any resin goes down. Contaminated tile beds, adhesive residues and degraded concrete all have to come out. Specialists profile the substrate with industrial diamond grinding and HEPA-filtered vacuum extraction. Chemical acid etching is avoided because it damages base concrete without opening a mechanical key.
Laying a new screed over greasy tiles guarantees early failure. The failed finish must be stripped back to sound concrete. Diamond grinding removes surface laitance, embedded oil and historic adhesive. That action opens the capillary pores so the resin primer penetrates the structure. Sealed vacuum units with HEPA filtration capture respirable crystalline silica at source. This protects building occupants and meets statutory dust exposure limits.

Need a Resin Flooring Site Visit and Quote?
Polyurethane Screed Specification for Lasting Traction
Aggregate Grading and Cleanability Trade-Offs
Engineered polyurethane screeds resolve slip hazards with graded quartz aggregate held through the cured matrix. Aggregate size is the balance point between traction and washdown efficiency. Staff need secure footing in heavy grease. The profile must not be so coarse that it traps soil and resists hygiene scrubbing.
A coarser profile delivers higher grip under heavy oil spills. An excessively rough floor shreds mops and holds food particles in deep surface valleys. Designers should specify the lightest grading that satisfies the site slip assessment. Installers must also check the safety data sheet and the product label. Where a product contains 0.1% or more diisocyanate, UK REACH requires training before professional or industrial use. That training must be repeated at least every five years.
Thermal Shock Resistance During Washdowns
Heavy duty polyurethane screeds tolerate continuous thermal cycling and sudden thermal shock. Boiling washdowns are routine work in catering. Rigid epoxy coatings crack and delaminate when scalded. FeRFA Type 8 polyurethane screeds flex with the concrete substrate and hold from roughly minus forty to plus one hundred and twenty degrees.
Standard epoxy expands and contracts at close to five times the rate of base concrete. Boiling water or a high-pressure steam lance across cold epoxy creates intense differential expansion. That shear strips the resin off the base. A 6 mm to 9 mm heavy duty polyurethane screed has a thermal expansion coefficient close to concrete. The system absorbs sudden temperature change without blistering, embrittlement or loss of adhesion.
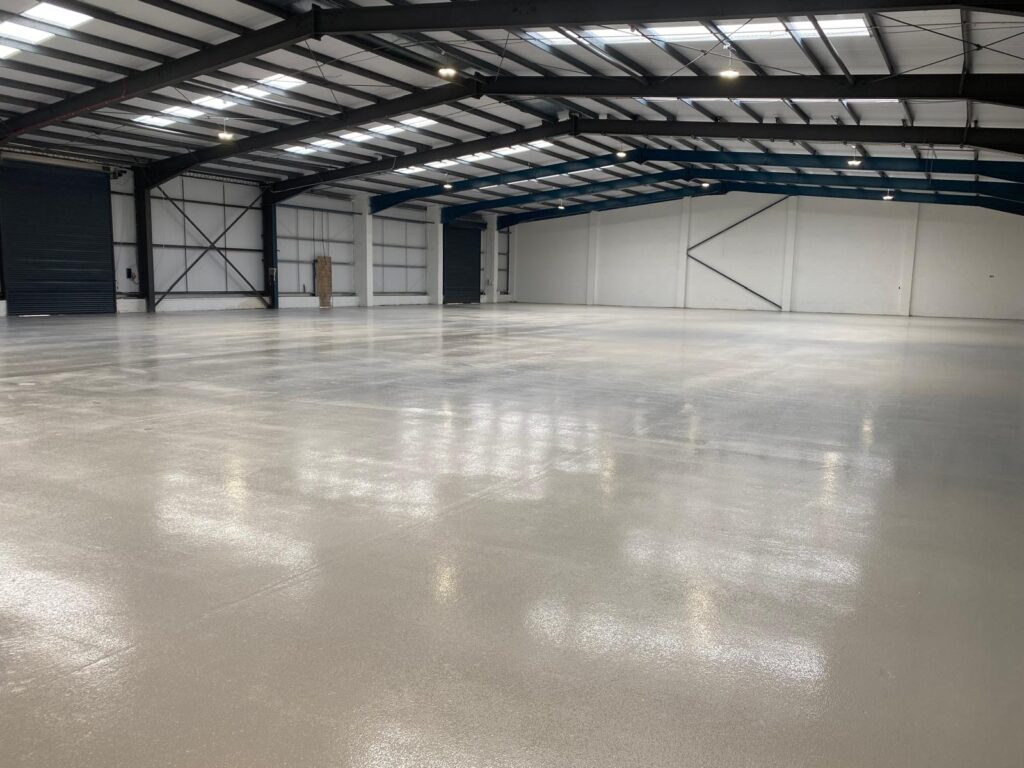
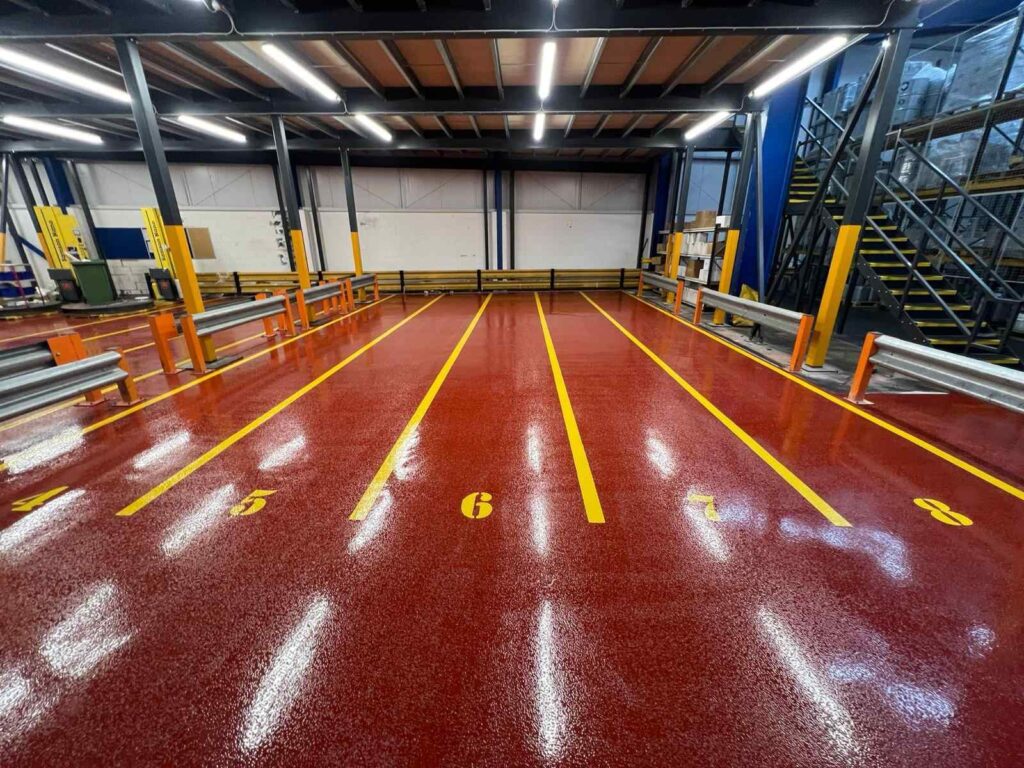
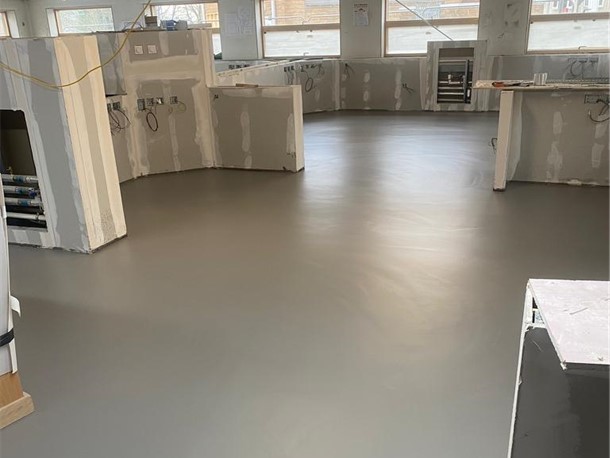
Case Studies
Our case studies cover – Printing & Packaging, Warehousing & Logistics, Pharma & Healthcare, Automotive & Engineering, Aviation & Aerospace, Food & Drink, Printing & Packaging, Warehousing & Logistics, Pharma & Healthcare
Compliance with UK Safety and Hygiene Legislation
Statutory Duties Under Workplace Safety Regulations
Regulation 12 of the Workplace (Health, Safety and Welfare) Regulations 1992 requires floors to be suitable, free from unevenness and not slippery. Section 2 of the Health and Safety at Work etc. Act 1974 adds a duty to safeguard staff. Known slip hazards must therefore be engineered out of the workplace.
The law treats an untreated, slippery kitchen floor as a continuing breach rather than a commercial fact of life. The 1974 Act obliges businesses to ensure safety so far as is reasonably practicable. Warning signs and safety footwear are personal protection. They sit at the bottom of the legal hierarchy of control. Employers must tackle the hazard at source with a surface engineered for predictable contamination.
Hygiene Mandates Under Regulation EC 852 2004
Regulation (EC) 852/2004 requires food preparation floors to stay sound and easy to clean. Surfaces must be impervious, non-absorbent, washable and non-toxic. Failing grout, cracked coatings and porous concrete all breach those requirements. Each one harbours pathogen reservoirs that routine disinfection cannot reach or sanitise properly.
Environmental health officers assess floor finishes closely at inspection. A surface that absorbs fat or cracks under traffic breaches food hygiene law. No flooring product can be HACCP certified. A resin floor can, however, be specified to meet the hygiene requirements of Regulation (EC) 852/2004. A seamless, non-porous polyurethane screed removes bacterial harbourage entirely. Water runs freely to collection points, which supports robust prerequisites for food safety management.
“JD Flooring did an excellent job installing a resin floor in our food production facility. The floor is durable, hygienic, and meets all safety regulations. The team was knowledgeable and professional, and the project was completed within the agreed-upon timeframe. I highly recommend JD Flooring for food industry flooring needs.”
Alex Martinez
Financial and Operational Ramifications of Neglected Floors
Enforcement Scales and Fee for Intervention
Slip incidents carry serious financial consequences under the health and safety sentencing guidelines. Where HSE inspectors identify a material breach, Fee for Intervention applies at £188 per hour from April 2026. Prosecution in the courts can then produce turnover-based unlimited fines for a commercial organisation.
Under the Definitive Guideline for health and safety offences, courts set fines from organisation turnover rather than profit. A high likelihood of harm can place a business in a severe sentencing band even with no actual injury. Starting points for a medium-sized enterprise run into hundreds of thousands of pounds. Dealing with floor defects early avoids enforcement notices, stop-work orders and substantial HSE cost recovery.
Downtime Costs Versus Lifespan Economics
Operational downtime usually costs far more than the floor itself. Low-cost topical fixes fail within months and force repeat closures. A professionally installed polyurethane screed delivers a service life of fifteen to twenty years. That lifespan cuts disruption and reduces total lifecycle expenditure across the building fabric.
Budgeting on first application cost hides the real expense of recurring failure. Re-coating a failing floor every winter means closing the kitchen, clearing equipment and losing trade. Heavy duty resin screeds for a commercial kitchen typically cost £70 to £100 per square metre installed. Spread across a fifteen-year life, that capital cost becomes a small annual figure. Avoiding one liability claim or emergency shutdown justifies the investment on its own.
Calculate The True Cost
A three day shutdown at a plant turning over £2,000 an hour is £120,000 of lost output. On most sites that is several times the cost of the new resin floor installation. We have developed our own free custom calculator top help you calculate the true cost and a new resin floor.
Permanent Remediation Process for a Slippery Kitchen Floor
Substrate Testing and Moisture Control
Permanent remediation starts with accurate substrate moisture assessment using calibrated hygrometers. Trapped damp creates osmotic blisters that lift an impermeable floor. Substrates showing high relative humidity need an impermeable liquid damp proof membrane. That barrier controls rising capillary moisture before the wearing screed is placed.
Concrete moisture destroys more resin floors than heavy traffic ever does. Residual ground moisture or trapped wash water raises vapour pressure under the new finish. That pressure forces the resin upward and creates brittle osmotic blisters. Technicians run relative humidity hygrometer tests across the floor area. Where readings exceed the resin tolerance, a two-coat epoxy liquid damp proof membrane suppresses moisture up to 98% relative humidity.
Drainage Gullies and Coved Skirting Detail
Correct detail work around stainless steel drainage gullies and wall perimeters removes the usual failure zones. Seamless coved skirtings turn the floor into an impervious vessel. Anchor grooves cut around drainage channels stop the edges lifting during hot water washdowns. Falls built into the screed keep liquid moving.
Floors fail at their terminations. Technicians cut mechanical anchor grooves parallel to every drain, gully and perimeter edge. The polyurethane screed keys into those slots and locks the edges against thermal contraction. Continuous radius-coved skirtings up walls and equipment plinths remove the ninety-degree dirt trap. Washdown water then flows to the drainage outlets instead of pooling along structural perimeters.
Final Thoughts
A resolved slippery kitchen floor changes daily safety, cleaning efficiency and regulatory standing. Replacing degraded quarry tiles with a heavy duty polyurethane resin screed attacks the cause of slip incidents. The surface holds consistent traction under viscous fat contamination. Moving away from mats and thin floor paints protects staff and removes bacterial harbourage at the same time.
Correct mechanical preparation, proper moisture mitigation and deliberate drainage detail produce a floor that performs under continuous commercial punishment. Engineering the hazard out at source leaves an audit-ready, hygienic environment built to sustain intense catering production for decades.
Arrange a Free Site Survey
If you are thinking about upgrading the flooring in your commercial or industrial space then we would love to hear from you. Our team of experts will conduct a free onsite survey and then guide you through the process of product selection and project planning, whilst remaining mindful of your budgetary restraints.
Frequently Asked Questions
A:
Clean water gives a misleading result because its viscosity is far lower than hot animal tallow, vegetable oil or emulsion-forming detergent. Microscopic surface roughness can cut through a thin water film and generate friction. Viscous cooking fat behaves differently. It forms a continuous lubricating layer that separates the sole from the floor texture completely. Accurate assessment of kitchen floor slip risk under BS 7976 therefore needs testing with the greasy contaminants encountered during service.
A:
Painting over worn tiles or a damaged substrate is a short-term measure that delaminates quickly. Standard floor paints and thin sealers measure a fraction of a millimetre. They cannot withstand dropped cookware, trolley wheels or aggressive washdowns. Paint also cannot bridge failing grout joints, and it will not adhere to oil-soaked surfaces. Effective remediation means removing the degraded coating, mechanically grinding the substrate and installing a resin screed that keys into the prepared base.
A:
Polyurethane screeds outperform epoxy on thermal shock tolerance and resistance to organic acids. Kitchens subject floors to boiling washdowns and steam cleaning as routine. Rigid epoxy expands and contracts at a very different rate from the concrete beneath it, which causes cracking and debonding. Heavy duty polyurethane screeds stay flexible from roughly minus forty to plus one hundred and twenty degrees Celsius. They also resist attack from lactic, citric and acetic acid.
A:
Standing liquid is both an immediate slip risk and a hygiene hazard under food safety law. Falls of 1:80 to 1:100 built into the screed push waste liquid into stainless drainage channels instead of leaving it in walkways. Integral coved skirtings at wall perimeters remove the sharp ninety-degree junction where fat, soil and water collect. Coving creates a seamless washdown-ready transition that allows thorough sanitisation and prevents moisture reaching the sub-floor.
A:
Slip incidents are prosecuted under the Health and Safety at Work etc. Act 1974 and Regulation 12 of the Workplace Regulations 1992. Health and safety breaches carry unlimited fines for businesses. Sentencing guidelines set penalties from company turnover and culpability rather than the severity of any actual injury. For large organisations, fines for high-culpability risks routinely start above one million pounds. The HSE also recovers inspection costs through Fee for Intervention at £188 per hour.
