
Anti-Static ESD Epoxy Floor: Resistance Windows
An anti-static ESD epoxy floor only works when it is specified as an electrical component. Uncontrolled electrostatic discharge destroys microelectronics, ignites solvent vapours and disrupts precision automation. Most procurement failures start with vague wording. A working static control floor needs a stated resistance to ground, verified surface preparation and a bonded connection to building earth.
Standard decorative resin behaves as an insulator. It generates triboelectric charge under foot traffic and wheeled plant, then holds that charge until it finds a path. So which resistance thresholds actually decide whether your resin floor complies with British and European standards?
Key Takeaways
- Specifying an ESD floor requires distinct electrical resistance windows rather than generic trade terms that fail technical audits.
- Conductive resin flooring operates between 10⁴ and 10⁶ ohms, whilst static dissipative surfaces discharge between 10⁶ and 10⁹ ohms.
- BS EN 61340-5-1 and EN 1081 govern test methods, requiring calibrated electrodes to measure resistance to ground accurately.
- Grounding continuity through embedded copper tape into verified building earth points remains mandatory for every electrostatic control floor installation.
- Substrate preparation by mechanical diamond grinding secures adhesion, preventing outgassing, pinholing and premature delamination across active production environments.
Electrical Classification Matrix for Industrial Flooring
Electrical resistance governs how quickly charge travels across a floor surface to earth. Standard resin systems act as insulators. They retain charge until an uncontrolled arc discharges into a sensitive assembly or an explosive vapour. Sorting systems into conductive, dissipative and insulating windows prevents expensive operational failure.
The table below sets out the resistance windows, governing standards and target environments seen across UK manufacturing. Specifiers should select the exact performance band named in their ESD control programme or their dangerous substances assessment. In practice, we find the band is often chosen after the coating has already been ordered.
| Classification | Resistance Range (Ohms) | Standard Reference | Primary Industrial Environment |
|---|---|---|---|
| ClassificationConductive | Resistance Range (Ohms)1 × 10⁴ to 1 × 10⁶ Ω | Standard ReferenceEN 1081 / DSEAR | Primary Industrial EnvironmentATEX zones, munitions, solvent stores |
| ClassificationStatic Dissipative | Resistance Range (Ohms)1 × 10⁶ to 1 × 10⁹ Ω | Standard ReferenceBS EN 61340-5-1 | Primary Industrial EnvironmentElectronics assembly, cleanrooms, data halls |
| ClassificationAnti-Static (Triboelectric) | Resistance Range (Ohms)Body voltage < 100 V | Standard ReferenceBS EN 61340-4-5 | Primary Industrial EnvironmentComponent handling, automated packing |
| ClassificationElectrical Insulating (LV) | Resistance Range (Ohms)> 5 × 10⁴ Ω (> 50 kΩ) | Standard ReferenceIEC 60364 | Primary Industrial EnvironmentSubstations and switchrooms under 500 V |
| ClassificationElectrical Insulating (HV) | Resistance Range (Ohms)> 1 × 10⁵ Ω (> 100 kΩ) | Standard ReferenceIEC 60364 | Primary Industrial EnvironmentHigh-voltage plant rooms above 500 V |

Terminology and Core Electrical Classifications
Conductive Versus Static Dissipative Flooring
Conductive resin floors carry the lowest resistance of any resin system. They move surface charge to earth almost instantly, measuring between 1 × 10⁴ and 1 × 10⁶ ohms. Static dissipative systems hold higher resistance. They bleed charge away steadily, between 1 × 10⁶ and 1 × 10⁹ ohms.
That distinction decides both personnel safety and component survival. Conductive floors suit solvent stores and pyrotechnic manufacturing, where any spark risk must be removed. Dissipative floors suit electronics benchwork. Slower dissipation protects operators from sharp discharge shocks whilst still preserving delicate semiconductor gates.
The Anti-Static Ambiguity in Specification Documents
The phrase anti-static describes a general property. It means reduced triboelectric charge generation, not a defined resistance window. Using the umbrella term in a contract invites installation error. Facilities then receive insulating coatings that resist initial frictional charging but leave live electronic components exposed to induction charges.
Industrial clients should drop ambiguous descriptors entirely. An engineering specification must state ohmic boundaries drawn from EN 1081 test protocols rather than product catalogue language. Without numerical criteria, a facility manager has nothing to verify at handover. From experience across the sector, that single omission causes most contested ESD floor installations.
Regulatory Standards and Verification Methods
BS EN 61340 Requirements for Electronics Manufacturing
BS EN 61340-5-1 sets the framework for protecting devices susceptible to electrostatic phenomena. The standard caps resistance to ground below 1 × 10⁹ ohms. It also requires that the combined person, footwear and flooring system keeps body voltage under 100 volts during normal movement.
Compliance depends on coordination, not on the floor alone. A compliant dissipative floor cannot earth an operator wearing standard insulating footwear. Verification therefore uses the walking test method in BS EN 61340-4-5. Technicians measure real-time voltage accumulated on an operator crossing the cured resin surface.
EN 1081 Resistance Testing Protocols
EN 1081 sets laboratory and site methods for determining vertical resistance and resistance to earth of floor coverings. Technicians use a tripod electrode fitted with conductive rubber pads. They apply a defined potential across the resin film. Testing then confirms whether the cured matrix meets the conductive or dissipative threshold.
Ambient conditions shift readings considerably. Technicians record relative humidity and temperature at every survey point, because dry air raises surface resistance. Handover documentation must carry the raw test logs. Those logs should show point-to-point and point-to-ground readings taken across each architectural bay.
Did You Know?
BS EN 61340-5-1 sets two hard numbers for an ESD protected area. Floor resistance to ground must stay below 1 × 10⁹ ohms, and body voltage on a walking operator must stay below 100 volts.
Operational Failure Modes and Common Specifying Errors
Opposing Technical Requirements Across Adjoining Rooms
Server rooms and high-voltage switchrooms need opposite electrical floor properties, yet they often share a dividing wall. Data halls need dissipative surfaces that move charge smoothly into earth terminals. Electrical distribution rooms need insulating floors under IEC 60364, preventing a shock path if a technician contacts a live phase.
Specifying one static control system across a whole technical building creates a genuine safety hazard. Conductive resin inside a switchroom forms a direct route to earth through an operator’s feet. Floor schedules must therefore be compartmentalised. Each partitioned zone is specified against its own functional duty.
Surface Contamination and Polish Incompatibility
Sacrificial waxes and protective polishes destroy the electrical performance of a dissipative resin system. Conventional maintenance emulsions dry as a non-conductive barrier. That microscopic film isolates traffic from the carbon pathways built into the resin matrix beneath, and the floor stops discharging altogether.
Introduce the wrong cleaning chemical and a compliant ESD epoxy resistance range climbs above 1 × 10⁹ ohms. Facilities should mandate pH-neutral detergents applied by scrubber-dryer with non-abrasive pads. Annual verification testing catches surface insulation early. Without it, the first symptom is usually unexplained component loss on the line.

Need a Resin Flooring Site Visit and Quote?
System Build and Sub-Floor Earthing Architecture
Copper Grid Integration and Grounding Terminals
An anti-static ESD epoxy floor cannot function without an engineered connection to structural building earth. Installers lay high-conductivity adhesive copper tape as an interconnected grid across prepared concrete. That grid goes down before the conductive coatings. The ribbons then route to dedicated grounding points fixed around the room perimeter.
A qualified electrical engineer must verify those terminals and connect them to the facility earth busbar. An unearthed conductive floor simply collects charge across its area. Where grounding connections fail or sit uncoupled, the floor behaves as a large capacitive plate. The discharge hazard then increases rather than falls.
Conductive Primers and Topcoat Formulations
Specialist ESD systems use a multi-layer composite build to hold conductivity through the full resin depth. Above the primer and copper grid, installers apply a black conductive intermediate coat loaded with carbon. That continuous layer carries charge horizontally across the whole floor plane.
The wearing topcoat contains dispersed conductive fibres or metal oxides. These transfer charge downward into the intermediate coat. Carbon additives darken clear epoxy binders, so ultra-light and pastel colours remain technically difficult. Specifiers should expect some colour variation when requesting decorative anti-static epoxy flooring.
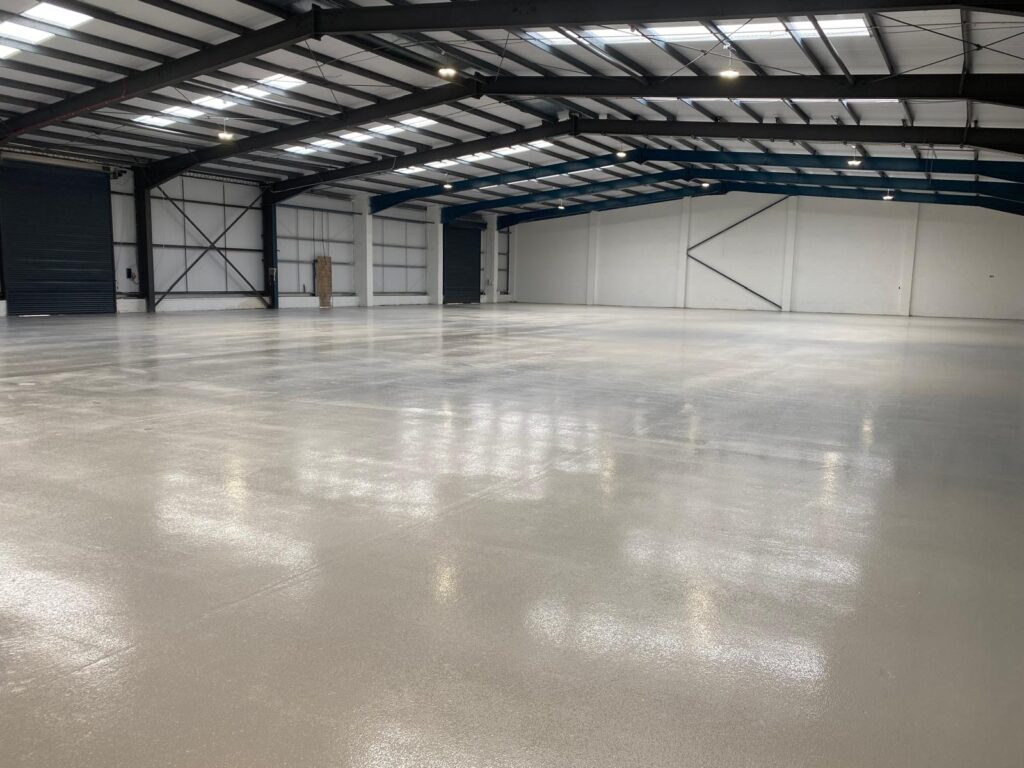
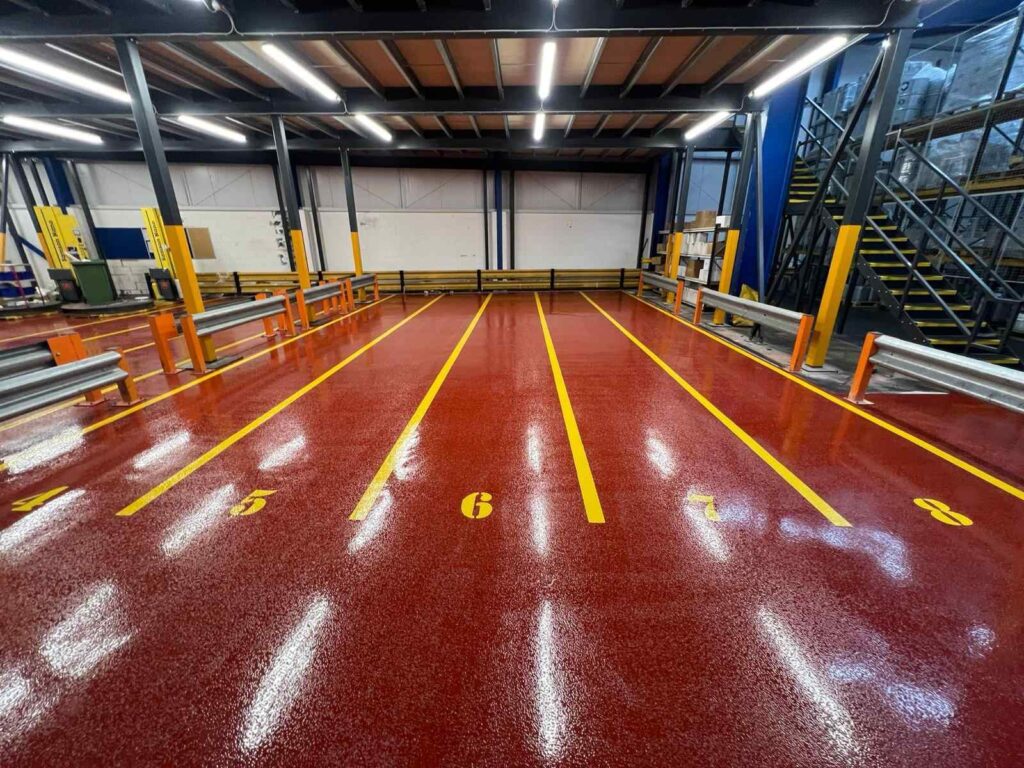
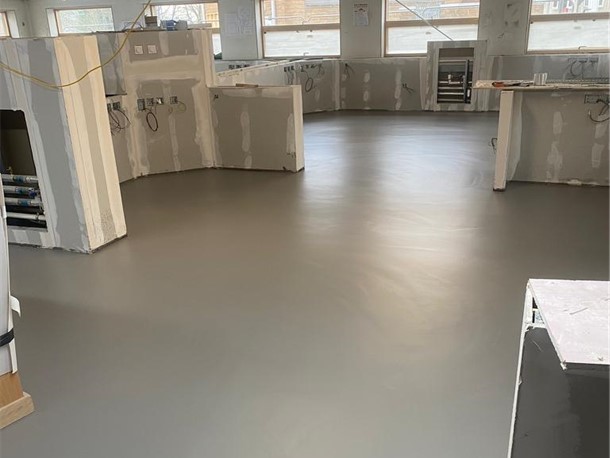
Case Studies
Our case studies cover – Printing & Packaging, Warehousing & Logistics, Pharma & Healthcare, Automotive & Engineering, Aviation & Aerospace, Food & Drink, Printing & Packaging, Warehousing & Logistics, Pharma & Healthcare
Substrate Preparation and Mechanical Profiling
Mechanical Diamond Grinding Protocols
A reliable bond starts with removing weak surface laitance by mechanical diamond grinding. Power-floated concrete presents a closed finish, so liquid resin cannot penetrate and anchor. Grinding opens the pore structure and leaves a clean, measurable profile. Industrial HEPA vacuums capture the fine particulate at source.
Dust control is a legal duty under COSHH, not site housekeeping. Concrete dust contains respirable crystalline silica, a Group 1 human carcinogen. The UK workplace exposure limit is 0.1 mg/m³ over an eight-hour shift. Contractors must run integrated on-tool extraction to suppress silica emissions throughout preparation.
Moisture Assessment and Vapour Suppression
Trapped moisture migrating up through concrete creates hydrostatic pressure. That pressure causes osmotic blistering beneath impermeable resin systems. Technicians must therefore run non-destructive moisture surveys with calibrated hygrometers before any ESD primer goes down. Standard epoxy systems generally tolerate substrate relative humidity up to 75 or 80 percent.
Where readings exceed that threshold, installers apply a two-coat epoxy liquid damp proof membrane. The suppression layer tolerates residual moisture up to 98 percent relative humidity. Skipping moisture testing invites widespread delamination. Delamination severs the embedded copper ribbons and destroys static dissipative continuity across the bay.
“JD Flooring did an excellent job installing a resin floor in our food production facility. The floor is durable, hygienic, and meets all safety regulations. The team was knowledgeable and professional, and the project was completed within the agreed-upon timeframe. I highly recommend JD Flooring for food industry flooring needs.”
Alex Martinez
Industrial Sector Applications and Risk Profiles
Electronics Assembly and Cleanroom Environments
Electronics manufacturers handle microprocessors and micro-electromechanical assemblies that suffer gate oxide damage below 100 volts. These environments call for self-smoothing dissipative resin, classified under FeRFA Type 5. A seamless surface stops particles lodging in cracks and supports compliance with ISO 14644-1 cleanroom cleanliness classes.
The finish must also survive a validated disinfectant regime. Specifiers choose chemical-resistant epoxy chemistries that tolerate repeated wipe-downs with isopropyl alcohol, biocides and rotating cleaning compounds. Integral coved skirting removes the floor-to-wall dust trap. It also makes sanitary cleaning far quicker for the production team.
Explosive Atmospheres and DSEAR Compliance
Sites handling flammable solvent vapours, aerosol lines or combustible powders fall under the Dangerous Substances and Explosive Atmospheres Regulations 2002. In zoned ATEX areas, an electrostatic spark carries enough energy to ignite an atmosphere. A conductive floor specification drains static potentials rapidly to earth instead.
Under DSEAR, employers must eliminate or control ignition sources across every classified zone. The floor forms part of that preventive engineering strategy. Failing to control explosion risk also breaches the Health and Safety at Work etc. Act 1974. Organisations then face unlimited fines under current sentencing guidelines.
Calculate The True Cost
A three day shutdown at a plant turning over £2,000 an hour is £120,000 of lost output. On most sites that is several times the cost of the new resin floor installation. We have developed our own free custom calculator top help you calculate the true cost and a new resin floor.
Cost Dynamics and Long-Term Asset Management
Initial Capital Spend Versus Operational Downtime
Industrial resin flooring typically runs from £8 to £45 per square metre. Thickness, preparation and conductivity requirements drive the spread. Basic coatings sit at the lower end, whilst multi-layer screeds and specialist ESD builds sit higher. Pricing stays indicative and remains subject to a formal site survey.
For high-throughput plants, lost output during installation usually dwarfs the flooring contract value. Fast-curing alternatives such as polyaspartic coatings or methyl methacrylate resins compress the programme when shutdown windows are tight. Project managers must still account for MMA odour taint near occupied production or commercial space.
Proactive Inspection and Lifecycle Maintenance
A professionally installed resin floor delivers 15 to 20 years of service when maintenance is scheduled. Neglect cuts that to between 5 and 7 years. Sweeping grit daily prevents the surface scratching that degrades slip resistance. The same abrasion also degrades measured electrical performance over time.
Annual condition surveys should document physical wear, arris spalling at expansion joints and any change in resistance to earth. Logged electrical audit records demonstrate active duty of care if component failures occur. Catching localised erosion early allows targeted bay recoating. That avoids the cost of full substrate re-preparation.
Final Thoughts
An anti-static ESD epoxy floor is an engineered electrical component, not a cosmetic finish. Specifiers must move past marketing language, fix the resistance window between conductive and dissipative performance, and prove earthing continuity through bonded copper ribbons. Correct diamond grinding with HEPA extraction then secures adhesion and protects the asset.
Static mitigation demands will tighten as semiconductor architectures shrink and automation speeds rise. Routine surface audits, strict cleaning chemical control and resin schedules aligned to zone risk keep production running. Balancing electrical thresholds, mechanical durability and maintenance protocol is what makes static protection hold across the full lifecycle.
Arrange a Free Site Survey
If you are thinking about upgrading the flooring in your commercial or industrial space then we would love to hear from you. Our team of experts will conduct a free onsite survey and then guide you through the process of product selection and project planning, whilst remaining mindful of your budgetary restraints.
Frequently Asked Questions
A:
Conductive floors measure between 10⁴ and 10⁶ ohms resistance to ground. They discharge electrostatic energy almost instantly. Static dissipative floors sit higher, between 10⁶ and 10⁹ ohms, and bleed charge away steadily rather than suddenly. Conductive systems suit solvent stores and ATEX zones where any spark must be eliminated. Dissipative systems suit electronics assembly, because controlled discharge protects both the components and the operator. The choice follows your ESD control programme or your dangerous substances assessment, never the product name.
A:
For an electronics assembly area or ESD protected area, BS EN 61340-5-1 requires resistance to ground below 1 × 10⁹ ohms. Most specifications target the dissipative band between 10⁶ and 10⁹ ohms. Where personnel grounding relies on the floor rather than wrist straps, the combined person, footwear and flooring system must keep body voltage under 100 volts during the standard walking test. Footwear and furniture therefore form part of the same compliance assessment as the resin itself.
A:
Charge has to travel somewhere safe, and a coating alone gives it nowhere to go. Installers embed a grid of high-conductivity copper tape directly beneath the resin and bond it to verified building earth terminals. A qualified electrical engineer confirms that connection at the earth busbar. Without those physical links, a conductive floor behaves as an insulated capacitive plate. It accumulates surface voltage across a large area and raises the discharge hazard rather than reducing it.
A:
Yes. Anti-static epoxy flooring needs pH-neutral detergents that leave no surface film. Conventional waxes, buffing polishes and sacrificial sealers form an insulating layer that blocks continuity to the conductive carbon matrix below. Resistance readings then rise outside the specified window, often without any visible change. Automated scrubber-dryers fitted with non-abrasive pads remove grit and spills without scoring the seal coat. Annual resistance testing confirms that the cleaning regime has not compromised electrical performance.
A:
No. Installing resin over excessive moisture causes osmotic blistering and debonding as vapour pressure pushes upward. Technicians must test concrete relative humidity with a calibrated hygrometer first. Standard epoxy systems tolerate roughly 75 to 80 percent relative humidity. Above that, a two-coat epoxy liquid damp proof membrane is required, suppressing residual moisture up to 98 percent. Skipping this step risks delamination that severs the copper earthing grid and destroys dissipative continuity.
