
Server Room Flooring: Static Control and Earthing
Server room flooring carries a duty no other floor finish does. It must drain electrostatic charge to earth before that charge reaches a network switch or a storage controller. A discharge of under one hundred volts can destroy a microprocessor gate without any person feeling a shock. The floor is the first line of defence.
Seamless resin systems remove the dust, vibration and loose joints that raised access tiles introduce. They also demand exact substrate preparation, a bonded copper earthing grid and verified resistance readings. Each of those three elements fails independently. So how should a technical team specify a floor that protects live infrastructure from electrostatic harm?
Key Takeaways
- Electrostatic protected areas require floor resistance to ground below one billion ohms under BS EN 61340-5-1 to safeguard network hardware.
- A server room floor coating laid over an unearthed substrate becomes an isolated conductive plane with no safe path for accumulated charge.
- Diamond grinding demands class H extraction, because respirable crystalline silica carries a workplace exposure limit of 0.1 milligrams per cubic metre.
- Commercial floor polish lays an insulating film that destroys the measured performance of a server room static dissipative floor within hours.
- Fast-cure polyaspartic resins accept foot traffic within two hours, letting technical teams resurface live comms suites across a single maintenance window.
Electrical Resistance Thresholds for Critical IT Floors
Resistance to ground decides whether a floor protects hardware or endangers people. Electrostatic protected areas need charge to leave the surface quickly. Electrical switchrooms need the opposite, because an insulating floor limits the current path through a technician’s body. Specifiers must therefore read the resistance window before they read the product datasheet.
The table below sets out the thresholds that govern resin selection in comms rooms and adjacent plant. Figures come from the British and international standards that apply in UK practice. Readings depend on test method, electrode weight and relative humidity, so certification must record those conditions alongside every result.
| Floor Classification | Resistance Requirement | Governing Standard |
|---|---|---|
| Floor ClassificationESD protected area floor (server room) | Resistance RequirementBelow 1 × 10⁹ Ω to ground | Governing StandardBS EN 61340-5-1 |
| Floor ClassificationConductive resin finish | Resistance RequirementBelow 1 × 10⁶ Ω | Governing StandardIEC 61340-4-1 |
| Floor ClassificationStatic dissipative resin finish | Resistance Requirement1 × 10⁶ Ω to 1 × 10⁹ Ω | Governing StandardIEC 61340-4-1 |
| Floor ClassificationPersonnel body voltage in an ESD protected area | Resistance RequirementBelow 100 V | Governing StandardBS EN 61340-5-1 |
| Floor ClassificationInsulating switchroom floor at 500 V or below | Resistance Requirement50 kΩ or above | Governing StandardIEC 60364-4-41 |
| Floor ClassificationInsulating switchroom floor above 500 V | Resistance Requirement100 kΩ or above | Governing StandardIEC 60364-4-41 |

Electrostatic Risk in Mission-Critical Environments
Triboelectric Charge Generation and Hardware Damage
Triboelectric charging happens whenever two materials touch and then separate. Foot traffic across unsealed concrete can generate several thousand volts on a person. People feel nothing below about three thousand volts. Modern semiconductors suffer gate oxide breakdown well under one hundred volts, so the damage threshold sits far below human perception.
In practice, these failures rarely announce themselves. Intermittent data drops and unexplained port resets get logged as software faults. Engineering hours disappear chasing the wrong cause. Seamless resin removes the friction sources that generate the charge in the first place. Loose carpet tiles, cracked vinyl planks and bare concrete all go. The main triboelectric generators under rolling equipment go with them.
Conductive and Dissipative Resistance Windows
Conductive systems measure below one million ohms and remove charge almost instantly. Dissipative systems sit between one million and one billion ohms, bleeding charge away at a controlled rate. Standard server halls specify dissipative finishes. The slower drain protects components whilst limiting the current that could pass through a person touching a live supply.
BS EN 61340-5-1 governs the measured outcome rather than the product alone. The standard treats flooring, footwear and personnel as one system. That system must hold body voltage below one hundred volts in normal operation. From experience across the sector, a compliant resin paired with ordinary rubber-soled work boots often fails the body voltage test. Footwear policy belongs in the specification alongside the resin.
Grounding Architecture and Earthing Grid Detail
Copper Grid Installation and Layout Rules
Earthing grids use flat high-purity copper tape laid straight onto the prepared concrete. Installers set the tape in perimeter bands or a cross-linked matrix spaced a few metres apart. The conductive primer then carries surface charge into that tape. Grid spacing and tape continuity decide whether the finished floor drains charge evenly or in patches.
Adhesion matters as much as layout. Installers anchor the ribbons with conductive adhesive backing, then join intersections with conductive eyelets or soldered points. Any loose tape lifts under the primer and shows later as a blister. When operating in this area, we check continuity along every run before the primer goes down. A break found at that stage costs minutes. The same break found after the topcoat costs the floor.
Verification Testing to Building Earth Points
A qualified electrical engineer must terminate the copper tapes into the building main earthing terminal or a clean IT earth. An unearthed conductive floor is worse than no treatment, because it spreads accumulated charge across a wider plane. Surface-to-ground and point-to-point resistance testing must follow termination, before any rack is commissioned.
Verification uses a calibrated megohmmeter with a weighted circular electrode. Engineers log readings in traffic aisles, at doorway thresholds and inside each equipment footprint. Relative humidity must be recorded with every reading, because a dry room reads higher. These first certificates become the baseline for annual audits. Without them, a later drop in performance cannot be attributed to wear, contamination or cleaning chemistry.
Did You Know?
Respirable crystalline silica carries a workplace exposure limit of 0.1 milligrams per cubic metre under HSE guidance note EH40/2005. The limit is averaged over an eight-hour shift. Diamond grinding without class H on-tool extraction can breach it within minutes.
Substrate Preparation and Moisture Protection
Mechanical Diamond Grinding Protocols
Diamond grinding opens the concrete pore structure, strips laitance and leaves an open texture for the resin to key into. Power-trowelled slabs carry a dense glassy skin that resists bonding and delaminates if coated directly. Grinding also levels the surface, removing undulations that would tilt a fully loaded cabinet.
Preparation dust contains respirable crystalline silica, classified as a Group 1 human carcinogen. Control falls under the Control of Substances Hazardous to Health Regulations 2002. On-tool extraction, class H vacuums and monitored filters are the minimum. In live comms rooms, we also shroud the work face and run negative pressure towards the extraction point. That keeps conductive concrete dust away from heat sinks and open rack apertures.
Vapour Drive Control with Liquid DPMs
Groundwater moves upward through a slab by capillary action and builds hydrostatic pressure beneath an impermeable resin. Where relative humidity readings exceed seventy-five per cent, a two-coat epoxy liquid damp proof membrane is required. Unmitigated vapour drive causes osmotic blistering. Blisters delaminate the resin and can sever the copper earthing bond underneath.
A liquid DPM suppresses moisture up to ninety-eight per cent relative humidity. It stabilises the slab before the conductive primer goes on. Where a cementitious levelling layer follows, installers broadcast fine quartz aggregate into the wet membrane to form a mechanical key. The result is a layered system that isolates the static control build from ground moisture. Adhesion holds, and so does the earth path.

Need a Resin Flooring Site Visit and Quote?
Retrofit Installation in Occupied Server Rooms
Airflow Management and Contamination Containment
Retrofitting a live comms room means protecting air-cooled switches from sub-micron particles. Contractors build negative-pressure airlocks and seal the supply air diffusers around the work zone. Grinding tools run with integrated HEPA extraction so dust is captured at source. Containment is a design task, not a housekeeping one, and it is priced accordingly.
Settled concrete dust conducts. On energised circuitry it can bridge adjacent traces and short a board. Cooling fans and heat sinks clog within hours in an uncontained room. Temporary shrouds around live racks are therefore standard practice, not an optional extra. Where a client refuses a shutdown window, containment is the only remaining control.
Fast-Cure Polyaspartic and Epoxy Systems
High-build epoxy needs up to forty-eight hours at fifteen degrees Celsius before it takes foot traffic. Fast-cure polyaspartic resins accept foot traffic in about two hours and reach full performance within twenty-four. That compressed window lets a technical team resurface a comms suite inside a single maintenance period.
Polyaspartic systems also cut solvent odour, which matters when adjacent offices stay occupied. They cure reliably down to minus five degrees Celsius, so a cold aisle holding temperature is no obstacle. Technicians apply several thin passes rather than one heavy coat. The finished server room floor coating then resists caster wear from heavy equipment without softening at the joints.
Case Studies
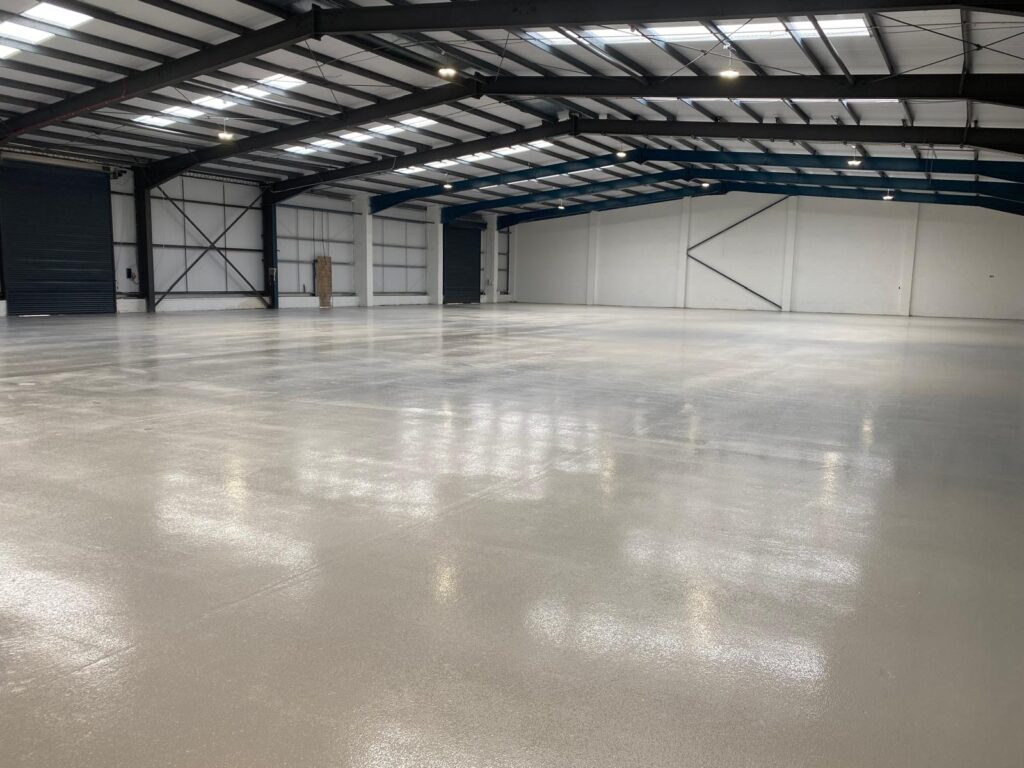
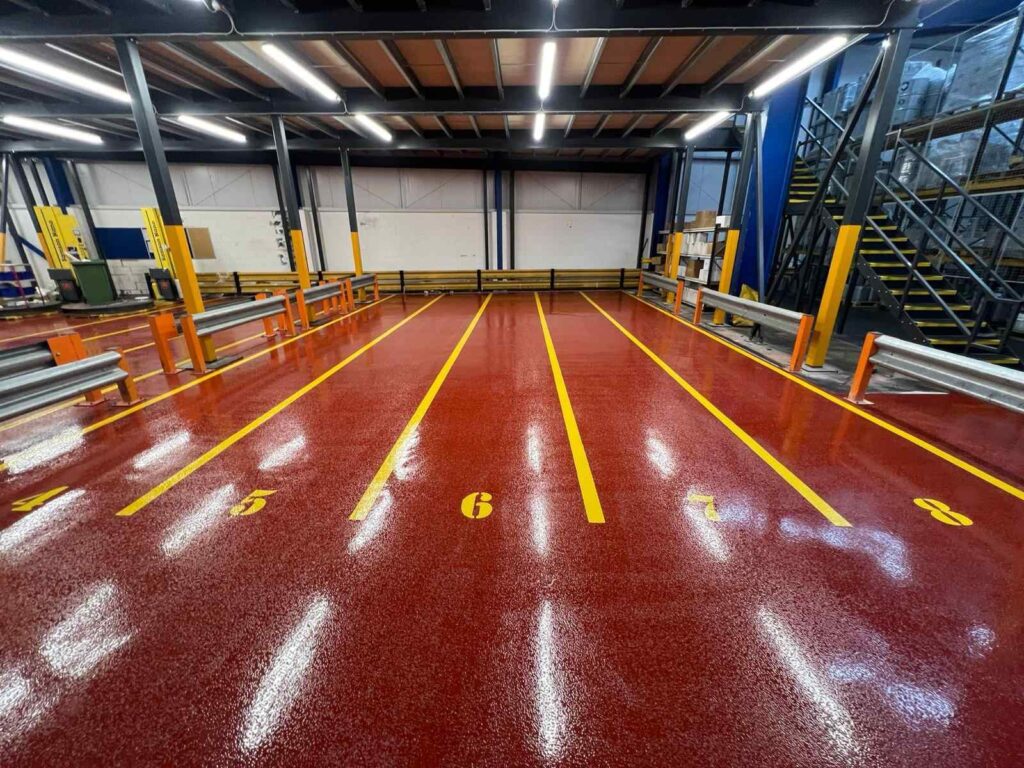
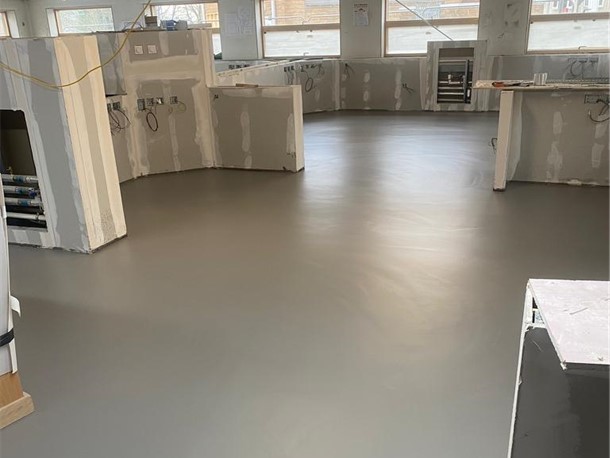
Our case studies cover – Printing & Packaging, Warehousing & Logistics, Pharma & Healthcare, Automotive & Engineering, Aviation & Aerospace, Food & Drink, Printing & Packaging, Warehousing & Logistics, Pharma & Healthcare
Resin Build Thickness and Point Load Resistance
Point Loading from Fully Populated Cabinets
A fully populated network cabinet concentrates its mass onto rigid casters and narrow levelling feet. Those contact points impose severe local pressure on the slab and the resin above it. A thin coating indents, and the indentation cracks the conductive layer. High-build formulations spread that load and keep the earthing traces intact.
Dragging a server chassis across a thin finish is the common failure we see. The damage shows as joint arris spalling, gouging and local debonding. Each gouge exposes the substrate and interrupts the measured earth path. Dropped hand tools do the same thing in a smaller area. A thicker build absorbs those impacts and keeps the certified resistance window intact.
FeRFA Build Classifications for IT Floors
FeRFA classifies resin floor finishes by build and performance, from thin coatings up to heavy-duty flowable systems. Server halls and comms rooms generally need Type 3 to Type 5, giving builds up to around four millimetres. Thinner classifications suit light traffic only and rarely survive rack installation.
Specifying by FeRFA type removes ambiguity from the tender. It fixes the build, not just the colour or the gloss level. Contractors then price comparable work, and the client can audit what was installed. In practice, we pair the FeRFA type with a stated resistance window and a named earthing detail. Those three lines settle most disputes before they start.
“JD Flooring did an excellent job installing a resin floor in our food production facility. The floor is durable, hygienic, and meets all safety regulations. The team was knowledgeable and professional, and the project was completed within the agreed-upon timeframe. I highly recommend JD Flooring for food industry flooring needs.”
Alex Martinez
Maintenance Practices That Compromise Conductivity
Insulating Waxes and Floor Polishes
Applying standard floor wax or acrylic polish to a conductive resin destroys its earthing performance. The emulsion dries as a dielectric film across the surface. That film blocks the path from a shoe sole down to the conductive body coats. Polished static control floors then fail routine resistance testing outright.
Cleaning contractors unfamiliar with ESD environments cause this failure whilst trying to improve gloss. Removing the acrylic needs chemical emulsification and abrasive scrubbing, which can scour the resin itself. The repair often costs more than the original cleaning contract. Signage at every comms room door is the cheapest control available. Name the approved products on it.
Approved Cleaning Chemistries and Regimes
Routine care means dry sweeping with a static-neutral microfibre mop, then light washing with a pH-neutral biodegradable detergent. Caustic cleaners strip the aliphatic topcoat. Heavy pine oils leave a surfactant film that interferes with discharge. The chosen solution must lift contamination without leaving any insulating residue behind.
Pad selection matters as much as chemistry. Aggressive rotary discs abrade the conductive carbon additives and erode the resin matrix. Service life shortens and resistance readings drift upward. A documented regime naming the mop, the detergent dilution and the pad grade keeps performance inside the certified window. It also gives the annual audit something to measure against.
Calculate The True Cost
A three day shutdown at a plant turning over £2,000 an hour is £120,000 of lost output. On most sites that is several times the cost of the new resin floor installation. We have developed our own free custom calculator top help you calculate the true cost and a new resin floor.
Floor Specification for Adjacent Switchrooms
Switchroom and Comms Room Conflict
Building layouts often place high-voltage switchgear in a plant room next door to a low-voltage comms suite. The comms room needs a dissipative or conductive floor to drain charge. The switchroom needs an insulating floor to limit current through a technician. One resin across both spaces breaches a fundamental safety principle.
IEC 60364-4-41 sets the insulating figures for a non-conducting location. Resistance must reach at least fifty thousand ohms at nominal voltages up to five hundred volts. Above five hundred volts the figure rises to one hundred thousand ohms. Those numbers are the opposite of an ESD specification. Reading one datasheet for both rooms is how the mistake usually happens.
Threshold Detailing and Earth Loop Control
The dissipative resin must stop at a defined line, normally the doorway threshold. Installers fit a physical demarcation there before the dielectric coating begins. A clean break prevents an unintended earth loop between the power distribution room and the communications hardware. The detail belongs on the drawing, not on the installer’s judgement.
Earth loops matter because a second path to ground can carry fault current where nobody expects it. Testing should cover both sides of the threshold separately. Record the readings against room numbers, not floor areas. From experience across the sector, the boundary is where certification most often falls apart. A single room number on a test certificate removes that ambiguity.
Final Thoughts
Specifying server room flooring means balancing three things at once: continuous static dissipation, mechanical durability and a verified earth path. The sequence runs from the slab upward. Moisture testing, diamond preparation and a bonded copper grid all precede the conductive topcoat. Skip one and the finish fails, however good the resin.
Maintenance then decides how long that performance lasts. An insulating wax undoes a six-figure installation in an afternoon. Audit the floor annually with calibrated instruments, log the humidity with every reading, and compare against the commissioning baseline. Rack density keeps rising, and the tolerance for electrostatic damage keeps falling.
Arrange a Free Site Survey
If you are thinking about upgrading the flooring in your commercial or industrial space then we would love to hear from you. Our team of experts will conduct a free onsite survey and then guide you through the process of product selection and project planning, whilst remaining mindful of your budgetary restraints.
Frequently Asked Questions
A:
Conductive finishes measure below one million ohms to ground and remove charge almost instantly. Dissipative finishes sit between one million and one billion ohms, draining charge at a slower, controlled rate. Most computer rooms and comms hubs specify dissipative systems. The slower drain still protects components. It also limits the current that could pass through a person touching a live low-voltage supply. The decision is a safety judgement as much as a hardware one.
A:
No. High-build resin needs a solid, stable concrete substrate. Access panels flex under caster loads, and a continuous resin laid across them cracks along every panel joint. The usual answer is to lift the raised floor and prepare the structural slab beneath it. Where the access floor must stay, replace damaged panels with factory-bonded static control vinyl or high-pressure laminate instead. Those panels are made for the movement that a poured resin cannot tolerate.
A:
They bond a grid of high-purity copper tape directly to the prepared substrate. Conductive primer and body coats then go over it. The tape runs terminate at earthing studs connected to the building's clean functional IT earthing terminal. A qualified electrical engineer makes that final connection. Engineers then test resistance to BS EN 61340-5-1 across the cured surface. They record readings in aisles, at thresholds and inside equipment footprints. Those results form the commissioning baseline.
A:
Commercial waxes and polishes contain non-conductive polymers and acrylic resins. Once dry, they sit as a thin dielectric layer over the resin surface. That layer blocks charge from reaching the carbon particles and the copper earthing grid embedded in the system below. The floor then fails electrical continuity testing, even though it looks better than ever. A certified ESD area becomes an uncontrolled hazard, and nothing on the surface shows it.
A:
Moisture rising through the slab builds hydrostatic pressure under a non-porous resin. The result is osmotic blistering and, eventually, total debonding. Moisture also corrodes the copper earthing ribbons, which severs the ground path and causes electrical failure. Testing with calibrated hygrometers before work starts tells you whether a liquid damp proof membrane is needed. Above seventy-five per cent relative humidity, specify one. The test costs little and the failure costs the whole floor.
