Data Centre Flooring: ESD Control and EN 1081 Testing
Mission-critical facilities fail in quiet ways. Electrostatic discharge degrades components long before anyone reports a fault. Specifying data centre flooring therefore means specifying an electrical system, not a surface finish. Resistance windows, earthing paths and cleaning chemistry together decide whether a floor protects hardware or quietly threatens it.
Charge builds under every castor and every footfall in a live server hall. Engineering teams must set the correct resistance window, prove it at handover, then hold it stable for years. So how should a specification define those limits, verify them under EN 1081, and protect them through the maintenance regime?
Key Takeaways
- Data centre static control flooring links conductive resin layers, embedded copper tape and the building earth into one continuous electrical path.
- BS EN 61340-5-1 requires resistance to ground below 1 × 10⁹ ohms across every protected area within the server hall.
- Switchrooms demand electrical insulation, not dissipation, so adjoining rooms often carry completely opposite flooring specifications either side of one wall.
- Handover acceptance depends on calibrated EN 1081 tripod testing at multiple grid positions, recording true electrical resistance to earth.
- Polymer floor polishes deposit insulating films that defeat static dissipation, so maintenance schedules must ban them for the service life.
Resistance Windows by Room Type
Electrical resistance requirements change room by room across a mission-critical site. A data hall needs controlled dissipation. A switchroom needs insulation. A hazardous-area store needs fast charge removal without ignition risk. Specifiers must therefore write separate resistance windows for each space, then hold the installer to the correct standard in every zone.
In practice, most handover disputes come from a single specification covering several room types. The table below sets out the governing standard and target window for each environment found on a typical campus. Use it to allocate chemistries at the physical threshold, before any resin reaches the concrete.
| Environment Type | Governing Standard | Target Resistance Window | Primary Safety Function |
|---|---|---|---|
| Environment TypeData hall (ESD protected area) | Governing StandardBS EN 61340-5-1 | Target Resistance WindowBelow 1 × 10⁹ Ω to ground | Primary Safety FunctionComponent protection and controlled charge bleed |
| Environment TypeData hall personnel grounding | Governing StandardBS EN 61340-5-1 | Target Resistance WindowBody voltage below 100 V | Primary Safety FunctionLimits charge carried by technicians |
| Environment TypeSwitchroom up to 500 V | Governing StandardIEC 60364-4-41 | Target Resistance WindowAbove 50 kΩ | Primary Safety FunctionOperator electric shock protection |
| Environment TypeSwitchroom above 500 V | Governing StandardIEC 60364-4-41 | Target Resistance WindowAbove 100 kΩ | Primary Safety FunctionOperator protection at higher voltages |
| Environment TypeHazardous area under DSEAR | Governing StandardIEC 60079-32-1 | Target Resistance WindowBelow 1 × 10⁸ Ω to earth | Primary Safety FunctionIgnition prevention through charge dissipation |

Performance Windows for Critical Server Facilities
Dissipative Thresholds for Component Safety
A dissipative data centre floor finish must hold electrical resistance to ground below 1 × 10⁹ ohms under BS EN 61340-5-1. That controlled conductivity bleeds accumulated charge away steadily. It avoids the rapid surge that destroys microprocessors, memory modules and the control electronics inside rack infrastructure.
Standard resin generates and stores charge. Rolling castors and pedestrian traffic are enough to do it. Dissipative formulations answer this by loading the resin matrix with conductive carbon fibres or carbonaceous fillers. Those additives run through the full depth of the wearing coat, so conductivity survives abrasion rather than sitting on the surface.
Insulation Demands in Electrical Switchrooms
Electrical switchrooms and high-voltage substations need insulation rather than dissipation. The floor protects personnel working on live equipment. IEC 60364-4-41 sets resistance to ground above 50 kilohms for systems up to 500 volts. Above 500 volts, that requirement rises beyond 100 kilohms.
A surface that safely bleeds static in a server hall becomes a shock hazard in a power distribution room. From experience across critical facilities, this boundary is drawn at the doorway. Each space receives its own chemistry, its own test regime and its own handover certificate.
Substrate Preparation and Moisture Mitigation
Mechanical Profiling for Bond Integrity
Resin installations need a clean, sound concrete substrate. Captive shot blasting or diamond grinding with HEPA extraction provides it. Removing laitance, curing agents and surface contaminants opens the concrete pores. The conductive primer can then interlock mechanically with the slab rather than bonding to a weak skin.
Resin floors mirror the profile of the concrete beneath them. Technicians inspect the prepared slab for cracks and joint arris defects. Structural resin compounds repair those defects first. An unyielding base must exist before any conductive element is laid.
Moisture Testing and Vapour Suppression
Engineers measure substrate moisture with a calibrated surface hygrometer before primers go down. Standard epoxies tolerate roughly 75 to 80 per cent relative humidity at the surface. Readings above that threshold call for a two-coat liquid damp proof membrane to prevent osmotic failure later.
Moisture vapour migrates upward through porous concrete. Hydrostatic pressure then builds beneath impermeable resin. Osmotic blistering follows, and it delaminates the conductive build-up. Ruptured earthing connections sit behind many of the static failures found during annual re-testing.
Did You Know?
Human Body Model Class 0 components, as classified under ANSI/ESDA/JEDEC JS-001, can be damaged by discharges below 250 volts. Most people cannot feel a static discharge until roughly 3,000 volts. A charge capable of destroying a Class 0 device therefore passes completely unnoticed by the technician carrying it.
Earthing Grid Design and the Conductive Matrix
Subfloor Copper Tape Network Layout
Installers embed a structured grid of high-conductivity copper tape across the primed slab. This happens before the conductive intermediate coat goes on. The tape links isolated bays into a continuous collector loop. Accumulated charge then has a defined route toward designated earthing terminals.
Layouts usually adopt a cross-hatch or perimeter grid. Spacing is set to keep resistance paths short across large floor plates. Technicians terminate the strips at grounding connection studs. A certified electrical engineer then tests those studs and ties them into the clean earth of the facility.
Conductive Resin Intermediate Primers
A conductive primer filled with carbonaceous additives goes directly over the copper array. This dark intermediate layer bridges micro-gaps between the slab and the tape. The result is a monolithic conductive plane. Charge arriving from the wearing coat passes into the grid without interruption.
Contact must be uninterrupted along the whole network. Skipped areas or poorly blended primer create isolated dead spots. Charge collects there with no exit path. Those spots rarely show up until EN 1081 testing records an out-of-range reading at handover.

Need a Resin Flooring Site Visit and Quote?
Testing Protocols and Handover Compliance
EN 1081 Test Methodology and Measurement
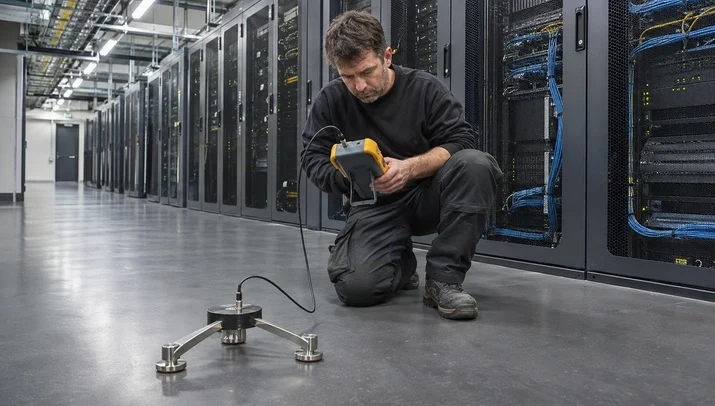
Handover verification uses the EN 1081 method to measure the electrical resistance of the installed floor covering. Technicians place a tripod electrode with conductive rubber feet on the surface. A defined compressive load simulates genuine pedestrian contact between footwear and the finished resin.
The instrument applies a DC test voltage across the electrode. Readings cover both vertical resistance and resistance to earth. Operatives must take multiple points in every distinct room zone. A single central reading proves nothing about perimeter bays or areas remote from an earthing stud.
Acceptance Criteria and Documentation Requirements
Acceptance requires every recorded reading to fall inside the specified BS EN 61340-5-1 window. Facilities managers should receive a full handover pack. That pack includes point-to-point resistance maps, resistance-to-earth results, ambient temperature logs, relative humidity data and signed earthing connection certificates.
Where the floor grounds personnel, specialists add body voltage generation tests to the EN 1081 work. The walking test confirms that an operator in compatible dissipative footwear stays below 100 volts in transit. Footwear and floor are tested as one system, because neither performs alone.
Case Studies
Our case studies cover – Printing & Packaging, Warehousing & Logistics, Pharma & Healthcare, Automotive & Engineering, Aviation & Aerospace, Food & Drink, Printing & Packaging, Warehousing & Logistics, Pharma & Healthcare
Durability, Chemical Resistance and Server Hall Demands
Point Loading and Rolling Castor Abrasion
Server halls carry severe mechanical loads. Rack cabinets, UPS battery frames and steel-wheeled dollies all concentrate weight onto small contact areas. A high-build resin or self-smoothing epoxy system provides the compressive strength required. The surface then resists indentation and cracking under sustained point loading.
Hard castors put intense shear stress on joint edges and perimeter transitions. A seamless installation removes grout lines entirely. Equipment then rolls smoothly during cabinet fit-out. Jarring is reduced, which matters when moving populated racks and sensitive optical media.
Zero Particulate Shedding and Air Purity
Uncoated concrete sheds fine mineral dust containing respirable crystalline silica as traffic abrades it. An impervious data centre floor finish seals the slab completely. Particulate shedding stops at source. Server air intake filters stay cleaner, and cooling units avoid the abrasive loading that shortens service life.
Cleanroom spaces and mission-critical halls demand near-zero dust generation. Conductive dust settling on a live circuit board can short it outright. Seamless resin finishes inhibit build-up and simplify precision cleaning. They also hold up under the air-handling regimes these rooms run continuously.
“JD Flooring did an excellent job installing a resin floor in our food production facility. The floor is durable, hygienic, and meets all safety regulations. The team was knowledgeable and professional, and the project was completed within the agreed-upon timeframe. I highly recommend JD Flooring for food industry flooring needs.”
Alex Martinez
Colour Limitations and Phased Refurbishment
Carbon Pigmentation and Shade Constraints
Carbon-based conductive additives darken every ESD resin system. That chemistry limits the available colour palette. Designers seeking bright, highly reflective white-space finishes must accept a darker undertone. Conductive fibres distributed through the resin matrix cannot be bleached out without losing electrical performance.
Shade matching across separate resin batches needs tight process control at manufacture. A standard colour range still covers most design schemes. Pale pastels, however, remain unrealistic in genuine static-control work. Specifiers should set colour expectations with the client before the sample stage, not after installation.
Refurbishment Sequencing Without Full Shutdown
Critical facilities rarely allow a complete shutdown for floor works. Fast-curing chemistries such as polyaspartic coatings make phased refurbishment possible. Work proceeds across isolated containment corridors or vacated equipment rows. Live servers avoid prolonged exposure to solvent vapour and extended programme disruption.
Technicians isolate active bays with temporary dust barriers and negative-pressure extraction during mechanical preparation. Fast-curing resin accepts foot traffic within hours. In practice, that speed is what makes a live-hall programme viable. It also keeps maintenance teams physically separated from operating data arrays.
Calculate The True Cost
A three day shutdown at a plant turning over £2,000 an hour is £120,000 of lost output. On most sites that is several times the cost of the new resin floor installation. We have developed our own free custom calculator top help you calculate the true cost and a new resin floor.
Lifecycle Maintenance and ESD Preservation
Floor Polish Contamination and Lost Conductivity
Applying sacrificial polymer wax or acrylic polish to an ESD floor destroys its electrical function immediately. These products dry to an insulating clear film. That film decouples the conductive resin matrix from footwear and equipment castors. Resistance readings then climb far outside the specified window.
Cleaning regimes must mandate pH-neutral detergents applied by scrubber-dryer with non-abrasive pads. Written instructions should name banned products explicitly. Contract cleaners change staff frequently, and a single tin of polish can undo an entire ESD installation. Routine scrubbing also removes grease films that raise resistance gradually.
Periodic Resistance Auditing and Verification
Facilities managers should run an annual test schedule with calibrated resistance meters. Wear patterns, abrasive traffic and chemical residue all shift surface characteristics over time. Formal records satisfy internal risk assessments and client service level agreements. They also prove the floor still performs as specified.
Condition surveys should assess surface wear, joint movement and point-to-ground continuity on high-traffic routes. Localised topcoat wear is cheap to address early. Left alone, it exposes the conductive layers and then the slab. Unplanned replacement in a live hall costs far more than planned maintenance.
Final Thoughts
Dependable data centre flooring is an electrical and structural system, not a cosmetic finish. Performance rests on mechanical preparation, moisture control, a continuous subfloor earthing grid and correctly applied conductive layers. Server halls and switchrooms pull in opposite electrical directions, and a competent specification separates them at the wall.
Long-term protection then depends on handover discipline and cleaning control. EN 1081 testing gives verifiable proof that an installation meets its design window on day one. Annual resistance audits and a standing ban on insulating polishes keep it there for the rest of the service life.
Arrange a Free Site Survey
If you are thinking about upgrading the flooring in your commercial or industrial space then we would love to hear from you. Our team of experts will conduct a free onsite survey and then guide you through the process of product selection and project planning, whilst remaining mindful of your budgetary restraints.
Frequently Asked Questions
A:
BS EN 61340-5-1 requires resistance to ground below 1 × 10⁹ ohms throughout an electrostatic discharge protected area. Where the floor also grounds operating personnel, the combined person, footwear and floor system must keep body voltage generation below 100 volts. Both figures matter. A floor can meet the resistance window and still fail the walking test if the footwear issued to technicians is incompatible with the surface specified.
A:
Server halls need dissipative surfaces that bleed accumulated charge away safely. Switchrooms need the opposite. Under IEC 60364-4-41, an insulating floor holds resistance to ground above 50 kilohms for systems up to 500 volts, rising beyond 100 kilohms above that. The purpose is operator shock protection, not component protection. Installing a conductive finish in a power distribution room creates a direct hazard for anyone working on live equipment.
A:
Contractors embed high-conductivity copper tape onto the prepared and primed slab before the conductive intermediate coats go down. The tape grid links the full floor area and terminates at dedicated earthing studs. A certified electrical professional then connects those studs into the clean earthing network of the building and tests the connection. The earthing certificate forms part of the handover pack, alongside the EN 1081 resistance results for each zone.
A:
Incorrect maintenance products are the commonest cause. Sacrificial polishes and acrylic waxes form an insulating film that blocks charge transfer entirely. Heavy accumulated grime produces the same effect more slowly. Mechanical failure of the copper earthing connections is the other main cause, often following osmotic blistering or substrate movement. Annual testing catches all three early, which is why a standing audit schedule matters so much.
A:
Standard epoxy and polyurethane systems usually accept light foot traffic within 24 to 48 hours. Full chemical cure and full compressive load capacity typically arrive between two and five days, depending on ambient temperature and humidity. Heavy racks and battery cabinets must wait for full cure. Rolling them across a partially cured floor risks permanent indentation, bond damage and disturbance of the conductive layers beneath.
